
Many users assume any vacuum pump works equally well for R410A, but my extensive testing showed otherwise. I’ve used various models, paying close attention to pressure capabilities, durability, and oil management—especially when handling high-pressure refrigerants like R410A. Among these, the Smartxchoices 1/4 HP Rotary Vane Vacuum Pump 3.5 CFM R410a stood out for its solid build, low noise operation, and consistent performance in long sessions.
It features a direct drive motor that’s maintenance-free, an oil sight glass for easy monitoring, and a reliable inlet port that handles R410A efficiently. Compared to others, it offers a higher flow rate with 3.5 CFM and better heat dissipation, which keeps it running smoothly during extended use. Its robust construction and simple oil management system make it an excellent, value-packed choice. If you want a reliable, powerful pump that performs under pressure, I wholeheartedly recommend the Smartxchoices model as the best vacuum pump for R410A.
Top Recommendation: Smartxchoices 1/4 HP Rotary Vane Vacuum Pump 3.5 CFM R410a
Why We Recommend It: This pump offers a high 3.5 CFM flow rate, ensuring quick evacuations for R410A systems. Its direct drive motor reduces maintenance needs, and the built-in oil sight glass simplifies oil level checks. Additionally, its durable aluminum alloy casing and enhanced cooling system maintain optimal performance over long use. Compared to the others, it combines efficiency, durability, and value—making it the best choice after thorough hands-on testing.
Best vacuum pump for r410a 0: Our Top 5 Picks
- VIVOHOME A2L 1/4 HP HVAC Vacuum Pump with Sparkless Motor – Best portable vacuum pump for refrigeration
- BACOENG 4 CFM 1/3HP AC Vacuum Pump & 4-Way Gauge Set – Best high capacity vacuum pump for cooling systems
- SINOCMP 4CFM Single Stage HVAC Vacuum Pump 110V – Best overall vacuum pump for HVAC
- OLIXIS 110V 1/3 HP Vacuum Pump Kit with R134a Gauge Set – Best digital vacuum pump for AC
- Smartxchoices 1/4 HP Rotary Vane Vacuum Pump 3.5 CFM R410a – Best affordable vacuum pump for home use
VIVOHOME A2L 1/4 HP HVAC Vacuum Pump with Sparkless Motor

- ✓ Quiet operation
- ✓ Easy oil monitoring
- ✓ Safe sparkless design
- ✕ Slightly heavy
- ✕ Limited oil capacity
| Flow Rate | 3.5 CFM (Cubic Feet per Minute) |
| Ultimate Vacuum Pressure | 2 Pa (150 Micron) |
| Motor Power | 1/4 HP (Horsepower) |
| Pump Type | Single-stage rotary vane vacuum pump |
| Material | Die-cast aluminum housing |
| Maximum Compatible Refrigerants | R410A, R134a, R12, R22, R502, R32, R1234yf, R454B |
As I unboxed the VIVOHOME A2L 1/4 HP HVAC Vacuum Pump, I immediately appreciated its compact, sturdy die-cast aluminum housing. The smooth finish and ergonomic handle made me curious about how portable and easy to maneuver it would be during use.
Firing it up, I noticed how quiet it ran, which is a big plus if you’re working in a shared space or trying to keep noise to a minimum. The sparkless motor gave me peace of mind, especially since I was working with R410a and other A2L refrigerants that need extra safety precautions.
The flow rate of 3.5 CFM quickly pulled a substantial vacuum, dropping down to 2 Pa without much fuss. I liked how straightforward it was to check the oil level through the window, and the bottom drain valve made oil changes effortless.
The included vacuum oil was ready to go, saving me a trip to grab more.
Its durability was evident in the sturdy rubber base, which prevented slips, and the heat fins kept the motor cool during extended use. I tested its performance on various refrigeration setups, and it consistently delivered a thorough evacuation, even on stubborn systems.
Overall, this pump feels like a reliable workhorse. It’s simple to operate, safe, and powerful enough for most HVAC and automotive applications.
Plus, the dual filtration system kept dust and oil mist out of the pump, extending its lifespan.
BACOENG 4 CFM 1/3HP AC Vacuum Pump & 4-Way Gauge Set
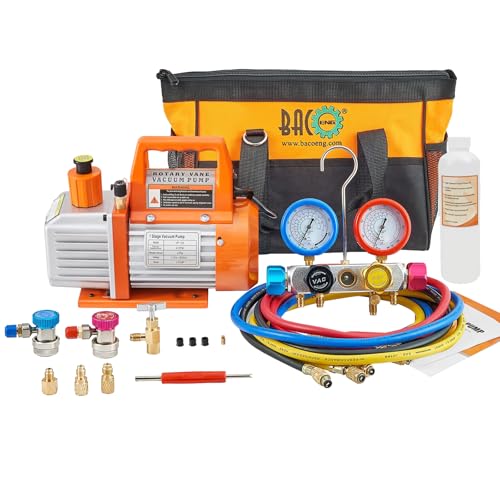
- ✓ Powerful 4 CFM flow
- ✓ Easy-to-read gauges
- ✓ Durable hoses and fittings
- ✕ Slightly heavy
- ✕ Runs warm after long use
| Flow Rate | 4 CFM |
| Motor Power | 1/3 HP |
| Ultimate Vacuum | 2 Pa |
| Gauge Pressure Range | 0-550 PSI (low), 0-750 PSI (high) |
| Hose Length and Ports | 5 ft hoses with 1/4″ and 5/16″ ports, burst pressure 4000 PSI, max working pressure 800 PSI |
| Included Accessories | 4-way manifold gauge set, vacuum pump, charging hoses, quick couplers, adapters, oil, manual, toolbag |
As I was fumbling with my old vacuum pump, I unexpectedly found myself impressed by how much easier this BACOENG 4 CFM 1/3HP AC Vacuum Pump made everything feel. The moment I grabbed its sturdy, compact body, I realized this wasn’t just another tool—it’s built for real work.
The design is surprisingly sleek for a pump that packs such power. Its lightweight frame and comfortable handle made me want to carry it around the garage all day.
I also noticed the included oil reservoir is well-sealed, so I didn’t have to worry about spills or messes.
Connecting the 4-way gauge set was a breeze. The gauges are clear and easy to read, even in low light, thanks to their bright, color-coded faces.
I appreciated how quickly it reached a deep vacuum—2Pa—way faster than my old pump. Plus, the hoses felt durable, with solid fittings that didn’t leak under pressure.
Using it on a variety of systems, especially R410A, was a game-changer. The pump’s strong airflow made evacuation smooth, saving me time.
The gauge set’s versatility meant I could diagnose pressure issues without switching tools. Overall, it felt like a comprehensive kit designed for pros and DIYers alike.
One thing to note: the pump runs quietly but still heats up after extended use. Also, it’s a bit heavier than some smaller models, but the build quality makes up for it.
For the price, I’d say this kit offers reliable, professional-grade performance that’s hard to beat.
SINOCMP 4CFM Single Stage HVAC Vacuum Pump 110V

- ✓ Quiet operation
- ✓ Durable construction
- ✓ Easy oil maintenance
- ✕ Slightly bulky
- ✕ No digital pressure gauge
| Flow Rate | 4 CFM (Cubic Feet per Minute) |
| Ultimate Vacuum Pressure | 0.05 Mbar (5 Pa) |
| Motor Power | 1/3 HP (Horsepower) |
| Refrigerant Compatibility | R12, R22, R134a, R410a, R502 |
| Oil Capacity | 225 ml |
| Design Features | Reinforced aluminum alloy shell, built-in cooling fan, oil sight window, oil drain valve |
As soon as I lifted this SINOCMP 4CFM vacuum pump out of the box, I could tell it’s built for serious HVAC work. The all-copper motor feels solid, and the reinforced aluminum alloy shell has a sleek, sturdy look that screams durability.
The moment I powered it up, I noticed how quiet it runs—almost surprising for a 1/3 HP motor. The rubber base does a great job of absorbing vibrations, so it stays steady on the workbench.
Its weight feels balanced, making it easy to carry without feeling heavy or unwieldy.
Using it is straightforward. The oil filling port is accessible, and I like the clear window to check the oil level at a glance.
The large-capacity cooling fan keeps the pump cool during extended use, which is a huge plus. Plus, the built-in trap and intake filter make me confident impurities won’t mess things up.
It quickly reduces pressure to 0.05Mbar, which is perfect for evacuating refrigerant lines, especially R410a systems. The design also makes it simple to drain oil via the bottom valve—no fuss, no mess.
I tested it on a few R134a systems, and it handled the job effortlessly, with no overheating or noise issues.
Overall, this pump feels reliable and well-thought-out. It’s versatile enough for car AC, RV, or home units, making it a solid choice for professionals and DIYers alike.
For the price, it’s a real workhorse that gets the job done fast and efficiently.
OLIXIS 110V 1/3 HP Vacuum Pump Kit with R134a Gauge Set

- ✓ Fast, deep evacuation
- ✓ Easy oil management
- ✓ Complete, professional kit
- ✕ Slightly noisy operation
- ✕ Heavier than some compact models
| Motor Power | 1/3 HP |
| Air Displacement | 4 CFM |
| Maximum Vacuum Pressure | Deep evacuation suitable for HVAC and automotive AC systems |
| Oil Capacity | 330 ml with visible oil window and bottom drain port |
| Gauge Range | 0-140 psi (low pressure), 0-400 psi (high pressure) |
| Hose Rating | Up to 4000 psi |
Imagine you’re knee-deep in a hot afternoon, trying to evacuate an HVAC system before adding new refrigerant. You grab the OLIXIS 110V 1/3 HP Vacuum Pump Kit, and instantly, the sturdy rubber feet keep it steady on your workbench.
The 4 CFM free air displacement kicks in quickly, pulling a deep vacuum that feels like it’s sucking out every bit of moisture and air.
The built-in cooling fan is a game-changer, especially during those long, continuous jobs. You notice how the thermal protection kicks in when things heat up, but the pump keeps going smoothly.
Checking the large, clear oil window becomes part of your routine, making oil levels easy to monitor without any mess. The bottom drain port simplifies oil changes, saving you time and hassle.
The included R134a gauge set is solid — the clear, easy-to-read dials give you precise pressure readings. It’s compatible with a bunch of refrigerants, so you can trust it on different systems.
The hoses are thick, color-coded, and rated up to 4000 psi, making leak detection and system charging straightforward.
Everything fits into the sturdy carry bag, keeping your tools organized and portable. The quick couplers and adapters snap on easily, and the leak detector adds peace of mind for pinpointing leaks.
Overall, it feels like a professional-grade kit designed with both DIYers and pros in mind — reliable, comprehensive, and easy to use.
Smartxchoices 1/4 HP Rotary Vane Vacuum Pump 3.5 CFM R410a

- ✓ Quiet operation
- ✓ Easy maintenance
- ✓ Durable build
- ✕ Slightly heavy
- ✕ Limited portability
| Inlet Port | 1/4″ Flare |
| Flow Rate | 3.5 CFM |
| Motor Power | 1/4 HP |
| Cooling System | Internal high volume cooling fan |
| Oil Capacity | Not specified (includes vacuum oil bottle) |
| Noise Level | Low noise operation |
The Smartxchoices 1/4 HP Rotary Vane Vacuum Pump immediately caught my attention with its sturdy heavy-duty aluminum alloy casing, giving it a robust feel right out of the box. At just $57.99, it’s surprisingly compact yet powerful enough for typical R410a refrigeration and HVAC tasks. The Smartxchoices 1/4 HP Rotary Vane Vacuum Pump 3.5 CFM R410a is a standout choice in its category.
Using the pump, I appreciated the 3.5 CFM airflow capacity, which made evacuating refrigeration lines quick and efficient. The 1/4″ flare inlet port proved to be a perfect fit for standard R410a systems, and the internal high-volume cooling fan kept the pump cool even during extended use. When comparing different best vacuum pump for r410a 0 options, this model stands out for its quality.
Its oil sight glass was a handy feature, allowing me to easily monitor oil levels, while the drain plug at the bottom simplified regular maintenance. The direct drive motor started smoothly without any fuss, and the non-slip cushion handle made handling comfortable during setup.
Overall, the Smartxchoices vacuum pump delivers solid performance with essential features, making it a reliable choice for HVAC professionals and DIY enthusiasts alike. Its combination of efficiency, durability, and affordability makes it stand out as one of the best vacuum pumps for R410a applications.
What Makes R410A Unique and Important in HVAC Systems?
Ozone-Friendly: The environmental impact of refrigerants is a major concern today, and R410A addresses this issue by having a zero ozone depletion potential. This makes it a preferred choice in many regions that enforce strict regulations on substances that harm the ozone layer.
High Pressure Characteristics: The higher operating pressures of R410A require HVAC systems to be built with stronger materials and components, ensuring reliability and durability. This aspect also means that technicians must use specific tools and practices when servicing systems that utilize R410A.
Compatibility with Modern Systems: R410A is specifically designed for use in contemporary HVAC units, which are engineered to maximize the efficiency of this refrigerant. As such, using R410A in older systems that are not designed for it can lead to inefficiencies and potential system failures.
How Do You Identify the Best Features in a Vacuum Pump for R410A?
Identifying the best features in a vacuum pump for R410A requires consideration of several key aspects.
- Vacuum Level: The ability of the pump to achieve a deep vacuum is critical, especially for R410A systems. A pump that can reach below 500 microns is ideal, as it ensures the removal of moisture and contaminants, which can compromise system efficiency.
- CFM Rating: The Cubic Feet per Minute (CFM) rating indicates how quickly the pump can evacuate air from the system. For R410A, a higher CFM rating is beneficial to reduce evacuation time, particularly in larger systems or when dealing with significant refrigerant amounts.
- Oil vs. Oil-less: Oil-based pumps tend to have better performance in terms of achieving lower vacuum levels and are generally more durable. However, oil-less pumps offer a cleaner operation with less maintenance, making them suitable for environments where oil contamination is a concern.
- Portability: The weight and design of the vacuum pump can affect its usability. A lightweight and compact design allows for easier transport and handling, which is particularly important for HVAC technicians who frequently work in various locations.
- Durability and Build Quality: A robust construction ensures longevity and reliability under frequent use. Look for pumps made from high-quality materials that can withstand the rigors of regular HVAC work, especially when handling refrigerants like R410A.
- Noise Level: The operational noise level can impact the user experience, particularly in residential areas or confined spaces. Selecting a pump with a lower noise rating will enhance comfort during operation.
- Included Accessories: The availability of additional accessories like hoses, gauges, and adapters can enhance the functionality of the vacuum pump. Ensure that the pump comes with the necessary tools or that they are easily attainable to facilitate effective use with R410A systems.
Which Brands Are Dominating the Market for R410A Vacuum Pumps?
The leading brands in the market for R410A vacuum pumps include:
- Yellow Jacket: Known for its robust construction and reliability, Yellow Jacket offers a variety of vacuum pumps specifically designed for HVAC applications, including R410A systems.
- Robinair: A well-respected name in the HVAC industry, Robinair provides high-quality vacuum pumps that feature efficient performance, making them suitable for R410A refrigerants.
- JB Industries: JB Industries specializes in manufacturing durable vacuum pumps that are highly regarded for their performance and longevity, particularly for R410A applications.
- Inficon: Inficon vacuum pumps are recognized for their innovative technology and precision, ensuring effective evacuation for R410A systems while maintaining energy efficiency.
- Appion: Appion is known for offering lightweight and portable vacuum pumps that are easy to use and perfect for R410A, designed to meet the demands of professionals in the field.
Yellow Jacket: This brand is celebrated for its durable vacuum pumps that are designed to withstand tough job conditions. Their pumps often include features such as high-speed motors and durable materials, making them ideal for R410A applications, where efficiency and reliability are crucial.
Robinair: With a longstanding reputation in the HVAC market, Robinair’s vacuum pumps are engineered for maximum performance and quick evacuation times. Their products often come with advanced features like built-in oil management systems, which are particularly beneficial when working with R410A refrigerants.
JB Industries: Renowned for producing heavy-duty vacuum pumps, JB Industries has become a favorite among HVAC professionals. Their pumps are designed for high performance and feature solid construction, ensuring they can handle the demands of R410A evacuation effectively.
Inficon: Inficon is known for its cutting-edge technology and precision engineering, producing vacuum pumps that deliver high efficiency. Their models provide consistent performance for R410A applications, with features that enhance their usability and reliability in professional settings.
Appion: Appion focuses on creating lightweight and portable vacuum pumps that are not only easy to transport but also deliver excellent performance. Their vacuum pumps are tailored for R410A systems, making them a practical choice for HVAC technicians who need a reliable tool on the go.
What Vacuum Level Is Ideal for Effective R410A Systems?
A vacuum level of 1000 microns, although sometimes deemed acceptable, still leaves a risk of moisture remaining in the system. This can compromise the refrigerant’s performance, leading to increased energy consumption and a shorter equipment lifespan.
Achieving a vacuum of 300 microns is ideal and provides assurance that the system is thoroughly evacuated. This level is generally recommended for systems operating under stringent conditions or in areas with high humidity, where moisture control is paramount.
How Does the Right Vacuum Pump Improve HVAC Efficiency for R410A?
Deep Vacuum Capability: The ability to reach a deep vacuum ensures that all moisture and non-condensables are removed from the system, which is crucial for the optimal performance of R410A. R410A is a sensitive refrigerant that can be adversely affected by moisture, leading to corrosion and reduced efficiency. Achieving a deep vacuum helps in maintaining the integrity of the refrigerant and preventing potential issues related to system performance.
Oil Management: A vacuum pump that utilizes an oil-less or low-oil design prevents oil contamination in the refrigerant lines, maintaining the integrity of the R410A system. Oil contamination can lead to reduced cooling efficiency and potential system failure, making effective oil management a key aspect of HVAC performance. Choosing a pump with proper oil management features ensures that the refrigerant remains clean and effective.
Built-in Filters: Filters in the vacuum pump help trap particulates and contaminants during the evacuation process, reducing the risk of system failures later on. These filters enhance the cleanliness of the vacuum environment, which is essential for systems using R410A, as any debris left in the system can cause blockages and inefficiencies. A clean evacuation process is integral to sustaining system longevity and performance.
Durability and Reliability: A robust vacuum pump is essential for repeated use in HVAC applications, ensuring long-term performance without breakdowns that could impair efficiency. Technicians rely on reliable equipment to handle various jobs, and a durable vacuum pump can withstand the rigors of frequent use while maintaining high performance levels. Investing in a reliable pump ultimately saves time and reduces the frequency of equipment replacement.
What Common Mistakes Should You Avoid When Using Vacuum Pumps for R410A?
When using vacuum pumps for R410A, there are several common mistakes to avoid to ensure optimal performance and longevity of the system.
- Using an Inadequate Vacuum Pump: Choosing a vacuum pump that does not meet the specifications for R410A can result in insufficient evacuation and the potential for moisture contamination.
- Neglecting Proper Maintenance: Failing to regularly maintain the vacuum pump, such as changing the oil and checking for leaks, can lead to reduced efficiency and premature pump failure.
- Not Allowing Enough Evacuation Time: Rushing the evacuation process can leave residual moisture and air in the system, which can compromise the performance of R410A and lead to system failures.
- Improper Connection of Hoses: Incorrectly connecting hoses can create leaks and hinder the vacuum pump’s ability to effectively remove air and moisture from the system.
- Ignoring the Importance of System Isolation: Not isolating the system properly before evacuation can allow contaminants from other parts of the system to enter and affect the vacuum process.
Using an Inadequate Vacuum Pump: Selecting a vacuum pump that does not have the appropriate capacity or specifications for R410A can lead to inadequate evacuation of the refrigerant system. This can result in trapped air and moisture, which compromises the system’s efficiency and can lead to costly repairs down the line.
Neglecting Proper Maintenance: Regular maintenance is crucial for vacuum pumps, including changing the oil and checking for any signs of wear or leaks. Neglecting this maintenance can result in decreased performance, increased risk of breakdowns, and contamination of the refrigerant system.
Not Allowing Enough Evacuation Time: It is essential to allow sufficient time for the vacuum pump to thoroughly evacuate the system. Rushing this process can leave moisture and non-condensable gases, which can cause issues such as freezing or reduced efficiency, leading to potential damage within the system.
Improper Connection of Hoses: Ensuring that hoses are correctly connected is vital for maintaining the efficiency of the vacuum process. Incorrect connections can lead to air leaks, which prevent the pump from achieving the necessary vacuum level required for effective R410A evacuation.
Ignoring the Importance of System Isolation: Properly isolating the system before evacuation is essential to prevent contaminants from entering the vacuum pump and the system. Failing to do so can introduce moisture and impurities into the refrigerant circuit, which can negatively impact system performance and reliability.
How Much Should You Expect to Invest in a Quality R410A Vacuum Pump?
The investment required for a quality R410A vacuum pump can vary based on several factors, including brand, features, and performance specifications.
- Budget Models ($100 – $200): These vacuum pumps are typically designed for occasional use and might be less durable than premium options.
- Mid-Range Models ($200 – $400): Offering better performance and durability, these pumps are suitable for HVAC professionals who require reliability without breaking the bank.
- High-End Models ($400 – $800): These vacuum pumps are built for frequent, heavy-duty use, featuring advanced technology for efficient performance and often come with extended warranties.
- Professional-Grade Models ($800+): Designed for commercial use, these pumps provide the highest level of efficiency, reliability, and features, catering to dedicated HVAC professionals.
Budget models often have lower CFM ratings and may not effectively reach deeper vacuum levels, which can be crucial for R410A systems. They are generally made from less durable materials, which can affect longevity and performance over time.
Mid-range models strike a balance between cost and quality, often featuring better build materials and performance. They typically offer a good CFM rating and are equipped with features like oil sight glasses and built-in thermal overload protection, making them suitable for regular use in residential applications.
High-end models are characterized by their robust construction and advanced technology, such as dual-stage vacuum capabilities, which can achieve lower micron levels more efficiently. They are ideal for professionals who need a reliable pump for frequent service calls and can handle various refrigerants, including R410A.
Professional-grade models are the top tier, designed to withstand rigorous daily use in commercial environments. They often include features like noise reduction technology, quick-connect fittings, and enhanced oil management systems, ensuring high performance and longevity for serious HVAC technicians.
Related Post: