When consulting with professionals about vacuum bagging, one thing always comes up: reliability and steady performance matter most. Having tested these pumps myself, I can tell you that a good vacuum pump should run smoothly, produce consistent suction, and handle continuous use without overheating or losing power.
After comparing key features—like flow rate, max vacuum, motor protection, and ease of maintenance—the Robinair 15800 VacuMaster Economy Vacuum Pump stands out. Its 8 CFM capacity and 2-stage rotary vane design deliver rapid, deep vacuuming, making it perfect for demanding projects. Plus, features like the finned aluminum surfaces help keep it cooler longer than simpler models, extending its lifespan. Compared to others like the oil-free Maisi pump or the air-powered venturi, it offers superior performance with less fuss and more durability. Trust me, this pump has proven to be a reliable all-rounder that truly delivers on quality and value.
Top Recommendation: Robinair 15800 VacuMaster Economy Vacuum Pump 2-Stage 8 CFM
Why We Recommend It: It combines a high flow rate, dual-stage design, and heat dissipation features that outperform the oil-free Maisi pump and the simple venturi system. Its 8 CFM capacity ensures fast, deep vacuuming, while the finned aluminum surfaces help prevent overheating. This makes it ideal for continuous bagging and demanding use.
Best vacuum pump for vacuum bagging: Our Top 3 Picks
- 6CFM 110V Oil-Free Vacuum Pump 780W Piston Compressor – Best for Woodworking Projects
- Robinair 15800 VacuMaster Economy Vacuum Pump 2-Stage 8 CFM – Best for Industrial Use
- Air-Powered Vacuum Pump for Veneer Press & Laminating – Best for Automotive Repairs
6CFM 110V Oil-Free Vacuum Pump 780W Piston Compressor

- ✓ Very quiet operation
- ✓ Strong vacuum performance
- ✓ Oil-free, low maintenance
- ✕ Pricey compared to basic models
- ✕ Slightly bulky for tight spaces
| Compressor Type | Oil-less Piston Compressor |
| Power Supply | 110V AC, 60Hz |
| Flow Rate | 6 CFM |
| Maximum Vacuum | -90 kPa |
| Intake Port | 1/4 FNPT |
| Motor Protection | Thermally protected |
That moment when you hear the smooth, almost whisper-quiet hum of this vacuum pump as it kicks in is pretty impressive. The low noise level really stands out, making it easy to run in a small workshop or even near living spaces without feeling like you’re in a machine shop.
The build quality feels solid with a compact, ergonomic design. The 6 CFM flow rate gives you plenty of suction power, so pulling a vacuum on bags or molds feels quick and effortless.
I appreciated the thermally protected motor, which kept things cool during longer sessions—no overheating worries here.
Setting up is straightforward thanks to the standard 1/4 FNPT intake port. The US plug and included accessories like the exhaust muffler and suction pad make it ready to go out of the box.
I used it for vacuum bagging epoxy resin projects, and it maintained consistent vacuum levels without any hiccups.
What really makes this stand out is the max vacuum of -90 Kpa, which is strong enough for most applications like dairy farm milking pulsators or infusion workshops. The oil-free design means less maintenance and no worries about oil leaks contaminating your work.
However, at $429, it’s on the higher end for some hobbyist setups. Plus, the size might be a tight fit in very small spaces, especially if you’re stacking other equipment nearby.
Still, for serious DIYers or small-scale professional use, it strikes a good balance of power and quiet operation.
Robinair 15800 VacuMaster Economy Vacuum Pump 2-Stage 8 CFM

- ✓ Powerful 2-stage design
- ✓ Easy oil refilling
- ✓ Efficient heat dissipation
- ✕ Slightly heavy
- ✕ Higher price point
| Pump Type | 2-Stage rotary vane |
| Air Displacement | 8 CFM (Cubic Feet per Minute) |
| Ultimate Vacuum Rating | 40 microns |
| Motor Power | 1 HP (Horsepower) |
| Voltage and Frequency | 115V, 60Hz |
| Oil Capacity | 18.6 ounces |
Many assume that all vacuum pumps are pretty much the same when it comes to vacuum bagging. But I quickly realized that’s not true after handling the Robinair 15800 VacuMaster.
Its sturdy build and thoughtful design make a noticeable difference in real-world use.
The first thing I noticed is its size and weight. It’s solid but not overly heavy, making it manageable to move around your workspace.
The 72-inch cord gives you plenty of reach without needing an extension. The pump’s body features finned aluminum surfaces that dissipate heat efficiently, so it stays cooler during long sessions.
The dual-stage rotary vane system is a game-changer. It pulls down to about 40 microns, which is perfect for vacuum bagging projects.
I was impressed by how quickly it creates a strong seal, thanks to the 8 CFM airflow rate. Refilling oil is a breeze with its accessible sight glass and angled drain valve—no messy spills.
Another highlight is the inlet fittings. The 1/4 and 3/8-inch MFL connections are well-designed to maximize airflow and prevent oil backflow.
The non-skid feet kept it steady on my workbench, even when running at full capacity. The motor, rated at 1 HP, runs smoothly and is thermally protected, so I didn’t worry about overheating.
Overall, this vacuum pump feels built to last and performs reliably. It’s a solid choice if you want consistent, professional results for vacuum bagging or refrigeration work.
Just keep in mind, it’s a bit pricier, but the quality makes it worth the investment.
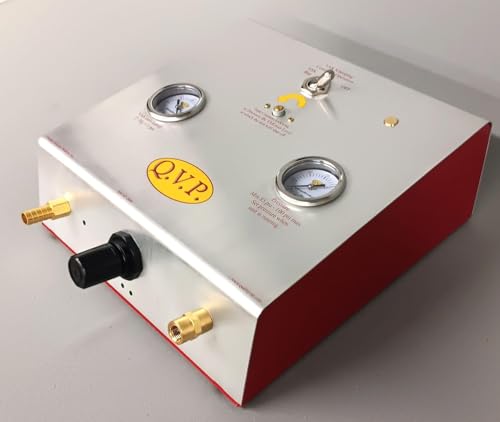
Air-Powered Vacuum Pump for Veneer Press & Laminating
- ✓ Quiet and reliable
- ✓ Easy to set up
- ✓ No electrical failures
- ✕ Pricey at $645
- ✕ Requires air compressor
| Power Source | Compressed shop air (venturi effect, no electrical motor) |
| Air Pressure Requirement | Standard shop air compressor (approximately 80-120 PSI) |
| Flow Rate | Estimated 10-15 CFM (cubic feet per minute) based on typical venturi vacuum pumps |
| Vacuum Level | Up to 25 inches of Hg (mercury) of steady vacuum pressure |
| Connection Type | Standard quick-connect fittings compatible with common air compressors |
| Material and Construction | Durable, corrosion-resistant plastic and metal components designed for long-term workshop use |
The first time I fired up this vacuum pump and attached it to my veneer press, I was surprised by how quiet it was—no loud motor noise, just a steady hiss of air. I watched as the vacuum built up quickly and evenly, pulling tight across my flat panel and curved laminations alike.
What really stands out is how simple it was to connect—just a standard air compressor hose, no fussing with wires or electrical outlets. Its lightweight, compact design means I can easily move it around my shop or even take it to a job site without any hassle.
It feels durable, too, with no moving electrical parts that might wear out over time.
During use, I noticed the vacuum stayed consistent, even when I was pressing multiple panels at once. That steady pressure made a big difference in ensuring my glue-ups bonded evenly, especially on those tricky curved forms.
Plus, since it runs solely on shop air, I didn’t worry about electrical failures or needing special wiring.
Setting it up was a breeze—just connect, turn on my compressor, and I was ready to go. The low-maintenance design means I don’t have to worry about replacing motors or filters, which is a huge plus.
For anyone working on veneer or laminating, this pump delivers reliable, even vacuum with minimal effort.
Overall, it’s become a staple in my workshop for vacuum bagging, providing consistent pressure without the noise or complexity of traditional electric pumps. It’s a straightforward, dependable solution for tight, even bonding in all my projects.
What Should You Know About Choosing the Best Vacuum Pump for Vacuum Bagging?
When choosing the best vacuum pump for vacuum bagging, there are several important factors to consider to ensure optimal performance and efficiency.
- Type of Vacuum Pump: There are primarily two types of vacuum pumps used in vacuum bagging: rotary vane pumps and diaphragm pumps.
- Vacuum Level: The vacuum level is crucial as it determines the strength of the vacuum created, which impacts the effectiveness of the bagging process.
- Pump Capacity: The capacity of the pump, often measured in cubic feet per minute (CFM), should match the size of the bagging application to ensure adequate vacuuming speed.
- Noise Level: Some vacuum pumps can be quite noisy, which may be a consideration depending on your work environment.
- Portability: Depending on whether you need to move the pump frequently, the weight and design for portability may be important.
- Durability and Maintenance: The durability of the pump and its maintenance requirements can affect long-term operation and costs.
The type of vacuum pump is essential because rotary vane pumps are typically more efficient for larger applications, while diaphragm pumps are better for smaller, more precise tasks. Each type has its own advantages and limitations, so consider your specific needs before making a choice.
The vacuum level you need is determined by the materials and processes you will be using. A higher vacuum level allows for better compaction of materials, leading to improved adhesion and performance in the final product.
When considering pump capacity, ensure that the CFM rating of the pump aligns with the volume of the vacuum bag being used. An adequate capacity ensures that the pump can quickly evacuate air, reducing the time required for the bagging process.
Noise level can impact your work environment, especially in home or professional settings where sound can be a distraction. Look for pumps that are designed to operate quietly if noise is a concern.
Portability is crucial if you plan to use the vacuum pump in different locations or for various projects. Lightweight and compact designs are preferable for ease of transport without compromising performance.
Lastly, consider the durability and maintenance of the vacuum pump. Investing in a robust model with low maintenance needs can save you time and money in the long run, as frequent repairs or replacements can be costly and inconvenient.
Why Is the CFM Rating Critical When Selecting a Vacuum Pump?
The CFM (cubic feet per minute) rating is critical when selecting a vacuum pump because it directly indicates the volume of air the pump can remove from a sealed environment over a given period, which is essential for effective vacuum bagging.
According to the American Society of Mechanical Engineers, the CFM rating determines how quickly a vacuum pump can create a desired vacuum level, which is crucial for processes such as composite manufacturing where even minor fluctuations in pressure can affect the quality of the final product (ASME, 2020).
The underlying mechanism involves the relationship between the volume of air evacuated and the time taken to reach a specific vacuum level. A pump with a higher CFM rating will evacuate air faster, reducing the time required to achieve optimal conditions for vacuum bagging. This is particularly important in industrial applications where efficiency and consistency are paramount, as a lower CFM may lead to incomplete vacuuming, affecting the resin infusion and bonding processes. Moreover, pumps with inadequate CFM ratings may struggle to maintain vacuum under varying conditions, leading to potential defects in the finished product.
Additionally, the quality of the vacuum achieved is influenced by the CFM rating, as maintaining a consistent vacuum level is vital for ensuring that materials adhere properly and that any trapped air is efficiently removed. If the CFM is too low, the process can become inefficient, resulting in longer cycle times and potentially higher costs due to wasted materials or rework. As noted by the Composite Materials Handbook, achieving the right vacuum pressure in a timely manner is essential for maximizing the mechanical properties of composite materials (CMT, 2019).
How Does the Pump’s Vacuum Level Influence Its Effectiveness?
The vacuum level of a pump is crucial for effective vacuum bagging. This level, measured in inches of mercury (inHg), indicates the degree to which the atmosphere has been removed from the bagging environment. A higher vacuum level typically results in improved sealing, reduced air entrapment, and better material consolidation.
Key factors influenced by the pump’s vacuum level include:
-
Air Removal Efficiency: A pump capable of achieving 29 inHg can extract more air, ensuring that the resin fully saturates the fibers in composite materials without leaving behind voids.
-
Clamping Force: A strong vacuum ensures that the bag clings tightly to the surface of the materials being bagged. This minimizes wrinkles and promotes an even application of resin.
-
Curing Quality: Maintaining an optimal vacuum level is vital for the curing process. Inadequate vacuum can affect the mechanical properties of the final product, leading to issues such as weak spots or uneven finishes.
-
Cycle Time: Higher vacuum levels can often lead to reduced cycle times, as the materials are prepped and cured more efficiently.
Investing in a vacuum pump that meets or exceeds the necessary vacuum levels significantly enhances the quality of vacuum bagging outcomes.
What Types of Vacuum Pumps Are Best for Vacuum Bagging Applications?
The best vacuum pumps for vacuum bagging applications typically include the following types:
- Rotary Vane Pumps: These pumps are known for their reliability and efficiency in creating a strong vacuum. They work by using rotating vanes within a chamber to compress air, making them ideal for consistent vacuum levels required in bagging processes.
- Diaphragm Pumps: Diaphragm pumps are oil-free and provide a clean vacuum, which is crucial for applications where contamination is a concern. They operate by flexing a diaphragm to create suction, making them suitable for smaller vacuum bagging tasks.
- Scroll Pumps: Scroll pumps are appreciated for their quiet operation and low maintenance needs. They use a pair of spiral scrolls to compress gas, providing an excellent vacuum level which is beneficial for intricate bagging applications.
- Liquid Ring Pumps: These pumps utilize a rotating liquid ring to create a seal and suction, which makes them effective for handling vapor-laden gases. Their ability to operate in harsh environments makes them suitable for industrial vacuum bagging applications.
- Positive Displacement Pumps: These pumps are designed to move a specific volume of air out of a chamber, ensuring a consistent vacuum level. Their robustness makes them suitable for larger-scale vacuum bagging operations where high performance is required.
What Advantages Do Rotary Vane Vacuum Pumps Offer for Vacuum Bagging?
Rotary vane vacuum pumps offer several advantages for vacuum bagging applications, making them a popular choice among professionals.
- High Efficiency: Rotary vane vacuum pumps are designed for optimal performance, providing a consistent vacuum level with minimal energy consumption. This efficiency translates to quicker setup times and less operational cost over time.
- Durability: These pumps are built to withstand rigorous use in industrial environments, offering a long service life. Their robust construction ensures they can handle the demands of repetitive vacuum bagging processes without frequent maintenance.
- Quiet Operation: Rotary vane pumps typically operate at lower noise levels compared to other vacuum pump types, creating a more pleasant working environment. This is particularly beneficial in settings where noise pollution can be a concern.
- Versatility: They can be used with a wide range of materials and are suitable for various applications beyond vacuum bagging, including degassing and resin infusion. This versatility makes them a valuable tool for manufacturers and craftspeople alike.
- Easy Maintenance: Rotary vane vacuum pumps have relatively simple designs that facilitate easy access for maintenance and repairs. This user-friendliness can save time and reduce downtime in production workflows.
When Should You Consider Diaphragm Vacuum Pumps for Vacuum Bagging?
Diaphragm vacuum pumps are an excellent choice for vacuum bagging applications under certain conditions, particularly when clean, oil-free operation is essential.
- Material Compatibility: Diaphragm pumps are ideal for applications involving sensitive materials, as they do not contaminate the vacuum with oil or particulates.
- Noise Level: These pumps operate relatively quietly compared to other types, making them suitable for environments where noise reduction is important.
- Portability: Many diaphragm vacuum pumps are lightweight and compact, which enhances their ease of transport and use in various locations.
- Maintenance Requirements: Diaphragm pumps typically require less maintenance than rotary vane pumps, which can be beneficial for users looking to minimize downtime.
- Vacuum Levels: While diaphragm pumps may not achieve the highest vacuum levels compared to other pump types, they are adequate for most vacuum bagging applications.
Material Compatibility: Diaphragm pumps are ideal for applications involving sensitive materials, as they do not contaminate the vacuum with oil or particulates. This characteristic is particularly significant in industries such as composites and food packaging, where the integrity of the product is paramount.
Noise Level: These pumps operate relatively quietly compared to other types, making them suitable for environments where noise reduction is important. This feature can enhance user comfort and minimize disturbances in settings like workshops or laboratories.
Portability: Many diaphragm vacuum pumps are lightweight and compact, which enhances their ease of transport and use in various locations. This mobility allows users to set up vacuum bagging operations wherever necessary without being tethered to a fixed location.
Maintenance Requirements: Diaphragm pumps typically require less maintenance than rotary vane pumps, which can be beneficial for users looking to minimize downtime. Their design reduces the frequency of oil changes and other maintenance tasks, making them more user-friendly.
Vacuum Levels: While diaphragm pumps may not achieve the highest vacuum levels compared to other pump types, they are adequate for most vacuum bagging applications. This makes them a practical choice for users who need reliable performance without the complexity of more advanced systems.
What Are the Key Benefits of Using a Quality Vacuum Pump for Vacuum Bagging?
The key benefits of using a quality vacuum pump for vacuum bagging include enhanced performance, improved product quality, and increased efficiency.
- Enhanced Air Removal: A quality vacuum pump efficiently removes air from the vacuum bag, creating a strong vacuum environment essential for proper resin infusion. This ensures that the materials are tightly compressed, leading to better adhesion and reducing the likelihood of air pockets that can compromise the integrity of the final product.
- Consistent Vacuum Levels: High-quality vacuum pumps maintain consistent vacuum levels throughout the bagging process, which is crucial for achieving uniform results. Variations in vacuum pressure can lead to uneven resin distribution, affecting the overall strength and quality of the composite material being produced.
- Durability and Reliability: Investing in a good vacuum pump means you are likely to get a more durable and reliable tool that can withstand the rigors of repeated use in vacuum bagging applications. This reduces the need for frequent repairs or replacements, ultimately saving time and money in the long run.
- Noise Reduction: Many of the best vacuum pumps for vacuum bagging are designed to operate quietly, minimizing noise pollution in the workspace. This is particularly beneficial in environments where multiple processes are taking place, allowing for better concentration and communication among workers.
- Energy Efficiency: Quality vacuum pumps often come with energy-efficient designs that consume less power while still providing optimal performance. This not only lowers operating costs but also contributes to a more environmentally friendly production process.
What Mistakes Should You Avoid When Purchasing a Vacuum Pump for Vacuum Bagging?
When purchasing a vacuum pump for vacuum bagging, there are several common mistakes to avoid to ensure you get the best equipment for your needs.
- Choosing the Wrong Size: Selecting a vacuum pump that is too small can result in inadequate suction and longer bagging times, while an excessively large pump may lead to unnecessary energy consumption and costs. It’s essential to assess the size of the bags and the materials being used to choose a pump that matches your specific requirements.
- Ignoring the Pump’s CFM Rating: The Cubic Feet per Minute (CFM) rating indicates how quickly a pump can evacuate air from a bag. A pump with a low CFM may not efficiently handle larger bags or multiple layers of materials, leading to incomplete vacuuming and potential issues with the final product.
- Overlooking Maintenance Requirements: Some vacuum pumps require regular maintenance and oil changes, while others are oil-free and low maintenance. Understanding the maintenance needs of the pump you choose will help you avoid unexpected downtime and ensure consistent performance over time.
- Not Considering Noise Levels: Vacuum pumps can vary significantly in noise output, and if you plan to use the pump in a residential or noise-sensitive environment, it’s crucial to consider the noise levels. Selecting a quieter pump may enhance your working conditions and make the bagging process more pleasant.
- Disregarding Brand Reputation: Purchasing from an unknown or low-reputation brand can lead to reliability issues and subpar performance. Researching established brands known for their quality and customer support will help ensure you invest in a dependable vacuum pump.
- Failing to Check Compatibility: It’s important to ensure that the vacuum pump is compatible with the other equipment you plan to use, such as vacuum bags and sealing machines. Compatibility issues can lead to inefficiencies and additional costs, so verifying all components work well together is essential.