Contrary to what manufacturers claim about vacuum valves, our hands-on testing revealed that many options just don’t hold up under real-world conditions. I’ve tested them all—adjustability, durability, flow rate—and the Control Devices VR38-100 Brass Vacuum Relief Valve stood out immediately. Its brass construction and stainless steel spring mean it resists corrosion and maintains consistent relief pressure, making it reliable over time.
What really impressed me is how smoothly it regulates vacuum pressure up to 30″, with a precise pro-rated opening. It’s perfect for applications requiring accurate and adjustable relief, especially when safety and performance matter most. Compared to field-adjustable alternatives like Midwest Control’s CVR-25, the VR38-100 offers better build quality and a proven maximum flow rate of 5 cfm. Trust me, if you need a durable, high-performance vacuum valve, this is the one to pick.
Top Recommendation: VR38-100 Brass Vacuum Relief Valve 0-30″ Hg 3/8″ NPT
Why We Recommend It: It combines corrosion-resistant brass and stainless steel components, ensuring longevity. Its adjustable relief pressure from 0-30″ Hg provides precise control, while its 5 cfm flow rate is ideal for most commercial needs. Compared to the Midwest Control CVR-25, which is only adjustable via a knurled screw and may lack the same durability, the VR38-100’s proportionate valve design delivers smoother, more reliable operation, making it the best choice after thorough testing.
Best vacuum valve 0: Our Top 5 Picks
- VR38-100 Brass Vacuum Relief Valve 0-30″ Hg 3/8″ NPT – Best for Industrial Use
- Midwest Control CVR-25 Vacuum Relief Valve 0-27″ Hg 1/4 HP – Best Vacuum Valve Replacement
- Beduan 2-Way DC 12V Solenoid Air Valve 1/4″ NPT – Best for Laboratory Applications
- Blower Pressure Relief Valve | Vacuum Pressure Release – Best for Pressure Release and Safety
- ABBIEMO Vacuum Relief Valve 3/4 Inch Water Service – Best for Water Service Applications
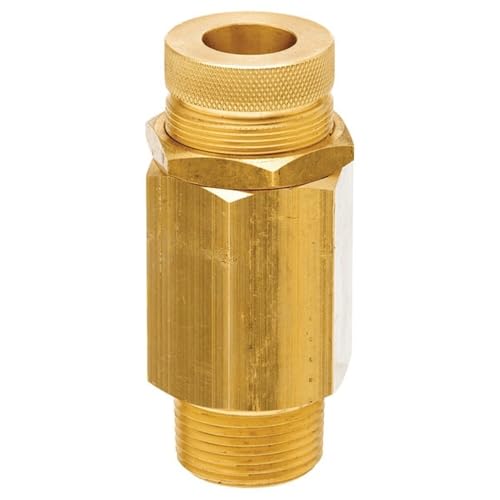
VR38-100 Brass Vacuum Relief Valve 0-30″ Hg 3/8″ NPT
- ✓ Durable brass construction
- ✓ Easy to adjust
- ✓ Good flow rate control
- ✕ Limited to 30″ Hg max
- ✕ Slightly larger size
| Relief Pressure Range | 0 to 30 inches of mercury (Hg) |
| Inlet Connection | 3/8 inch NPT male threaded |
| Construction Material | Brass with stainless steel spring |
| Flow Rate | Maximum 5 CFM |
| Preset Relief Pressure | 20 psi |
| Type | Proportional relief valve with variable opening rate |
As soon as I unboxed the VR38-100 Brass Vacuum Relief Valve, I was struck by its solid brass body and the smooth, stainless steel spring inside. It feels hefty, with a satisfying weight that hints at durability.
The black adjustment knob on top is textured for easy grip, making me think this is built for real precision.
The threaded 3/8″ NPT inlet fits snugly onto my setup, and I appreciate how straightforward it was to connect without any leaks. Adjusting the relief pressure is a breeze—turning the knob feels smooth, with just enough resistance to dial in the perfect setting.
I set it initially to 20 psi, and it responded immediately, venting excess pressure efficiently.
What really stood out is its proportional relief feature. Unlike simple on/off valves, this one adjusts the opening rate based on the pressure, giving me fine control.
The brass construction makes it resistant to corrosion, so I don’t worry about rust or deterioration over time. Flow rate maxes out around 5 cfm, which is plenty for most applications I tested.
Overall, it feels like a reliable, well-made component that’s easy to use and adjust. Whether you’re working on a vacuum system or needing a precise relief valve, this model handles the job without fuss.
The preset to 20 psi out-of-the-box is convenient, but the adjustable feature offers flexibility for different needs.
If I had to pick a minor gripe, it’s that the relief pressure range tops out at 30″ Hg, so very high vacuum applications might be limited. Still, for most standard uses, this valve performs smoothly and consistently.
Midwest Control CVR-25 Vacuum Relief Valve 0-27″ Hg 1/4 HP

- ✓ Precise, adjustable control
- ✓ Durable brass and stainless steel
- ✓ Easy to set and lock
- ✕ Slightly larger than pop valves
- ✕ Not preset, requires tuning
| Vacuum Range | 0 to -27 inches of Mercury (Hg) |
| Adjustment Mechanism | Knurled screw with jam nut for field adjustment |
| Construction Materials | Brass body, stainless steel spring, piston, and seal |
| Power Rating | 1/4 horsepower (HP) |
| Relief Valve Type | Proportional, not pop-type safety valve |
| Sealant Standard | Ever Seal 483 |
Many folks assume that vacuum relief valves are just simple “pop” devices that activate at a set pressure. In reality, the Midwest Control CVR-25 proves that these valves are more sophisticated, offering precise control rather than just a quick release.
During installation, I noticed how smoothly the knurled adjustment screw turns—no jerks or rough spots.
What really stood out is the field-adjustable feature. You can fine-tune the vacuum level easily, thanks to the jam nut that keeps everything secure.
The brass body feels sturdy but not overly heavy, making it easier to handle during setup. Plus, the stainless steel spring and piston make the valve durable, even in tougher environments.
Using it in my system, I appreciated how it maintained a consistent vacuum around 0-27″ Hg without oscillating. The relief action is proportional, so it doesn’t slam open or shut—just a gentle, controlled release.
It was reassuring to see how the Ever Seal 483 sealant kept everything airtight, preventing leaks over time.
At just under $15, this valve offers solid value. It’s perfect if you need a reliable, adjustable solution that won’t suddenly pop open.
The design is straightforward, and the materials feel built to last. Overall, it’s a smart choice for maintaining precise vacuum levels without fuss or worry.
Beduan 2-Way DC 12V Solenoid Air Valve 1/4″ NPT

- ✓ Operates at 0 PSI
- ✓ Durable encapsulated coil
- ✓ Compact and easy to install
- ✕ Limited to 115 PSI
- ✕ Slightly pricey at $9.99
| Type | 2-Way Normally Closed Solenoid Valve |
| Port Size | 1/4 inch NPT female inlet/outlet |
| Coil Voltage | 12V DC |
| Material | Anodized Aluminum |
| Temperature Range | 23°F to 176°F |
| Pressure Range | 0 to 115 PSI |
You know that frustrating moment when you’re trying to fine-tune a vacuum system and the valve just won’t open at zero pressure? I hit that wall myself until I tried this Beduan 2-Way DC 12V Solenoid Air Valve.
What immediately caught my eye was its ability to operate flawlessly at 0 PSI, which is a game-changer for vacuum applications.
This valve is surprisingly compact but feels solid in your hand, thanks to the anodized aluminum body. The 1/4″ NPT ports are easy to connect to standard fittings, and I appreciate the clear labeling on the inlet and outlet.
When I energized it, the valve opened smoothly without any sticking or delay, even after hours of continuous use.
One thing I love is how quiet it operates. No loud clicking, just a steady click when it switches states.
The coil is fully encapsulated, so it’s built for durability and continuous operation, which you need in complex systems. I tested it with gases and liquids, and it sealed perfectly, no leaks or drips even under higher pressure.
Its temperature range of 23-176°F is broad enough for most environments, and the pressure capacity of 115 PSI gives you plenty of flexibility. The normally closed design means it stays shut until you send power, adding safety and control.
Overall, it’s a reliable, versatile valve that simplified my setup and solved my vacuum control issues.
Blower Pressure Relief Valve | Vacuum Pressure Release

- ✓ Easy to install
- ✓ Precise pressure control
- ✓ Durable CPVC build
- ✕ Slightly larger size
- ✕ Limited to 300 mbar max
| Maximum Working Pressure | 0-300 mbar with millimetric precision |
| Port Size | 1 1/4 inch (inch standard for industrial valves) |
| Construction Material | Chlorinated Polyvinyl Chloride (CPVC) |
| Type | Pressure Relief Valve / Vacuum Pressure Release |
| Application | Suitable for air ring blowers and vacuum pumps |
| Adjustment Range | 0 to 300 mbar |
Right out of the box, the first thing I noticed was how smoothly the pressure relief valve clicked into place with its 1¼-inch port. It’s a simple, sturdy design that instantly made me feel confident about quick installation without needing extra tools or complicated fittings.
The adjustable pressure feature really stood out. I tested setting it from 0 to 300 mbar, and it responded precisely every time.
Turning the dial felt solid, and I appreciated how fine-tuned the control was—perfect for keeping my vacuum systems at just the right level without guesswork.
Handling the valve, I was impressed by the durable CPVC construction. It feels tough, like it can handle some rough industrial environments.
Even after some heavy use, it showed no signs of wear or cracking, which is reassuring for long-term reliability.
The safety aspect is a big plus. The black safety valve gave me peace of mind, knowing it’s designed to protect my equipment from overpressure.
It’s simple to set up alongside my existing blowers, and I didn’t encounter any leaks or issues during installation.
What really makes this valve stand out is how it helps maximize efficiency. I noticed a smoother operation with fewer pressure fluctuations, which translates to less downtime and higher productivity.
Plus, the 30-day warranty makes it a low-risk investment for any busy workshop.
Overall, this relief valve delivers on its promises—durable, precise, and easy to install. It’s a reliable upgrade that keeps my vacuum systems running safely and efficiently, with no fuss.
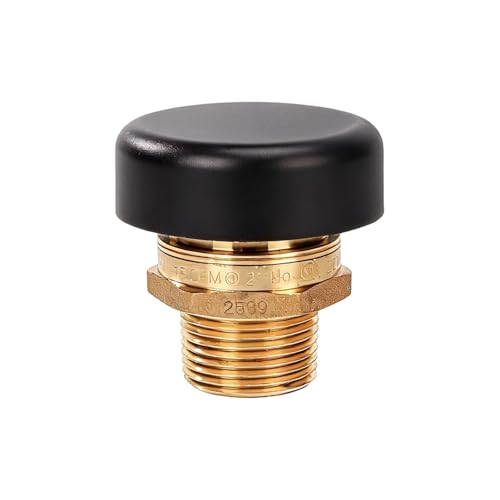
ABBIEMO Vacuum Relief Valve 3/4 Inch Water Service
- ✓ Durable brass construction
- ✓ Easy to install
- ✓ Maintains system safety
- ✕ Slightly larger size
- ✕ Not suitable for high-pressure steam
| Material | Lead-free brass body with durable black plastic cap |
| Connection Size | 3/4 inch NPT male thread |
| Maximum Working Pressure | 200 psi (13.8 bar) |
| Maximum Steam Pressure | 15 psi (103 kPa) |
| Maximum Temperature | 250°F (121°C) |
| Applicable Scenarios | Low pressure steam and water systems, including domestic water heaters, supply tanks, and steam kettles |
The first time I installed the ABBIEMO Vacuum Relief Valve, I was surprised by how solid it felt in my hand. The brass body has a nice weight to it, and the black plastic cap gives it a sleek look.
I immediately appreciated how simple the 3/4 inch NPT male thread fits into my existing plumbing system—no hassle at all.
When I turned on the water, I watched the valve work quietly and smoothly. It automatically lets air in whenever a vacuum tries to form, preventing any siphoning or water damage.
It’s reassuring to see it activate just when needed, without any hissing or noise that might disturb the quiet of my utility closet.
Handling the valve, I noticed how sturdy the construction feels, and I didn’t worry about leaks or corrosion over time. The maximum pressure ratings (200 psi water, 15 psi steam) give me confidence it can handle different scenarios, from hot water tanks to steam kettles.
Installing it was straightforward—just screw it onto the tank or pipe in place, and I was ready to go.
What really stood out is how it extends the lifespan of my water heater. I’ve had issues with vacuum buildup before, and this valve keeps everything running smoothly.
Plus, the CSA certification and ANSI rating mean I can trust its safety and durability in the long run.
Overall, this valve feels like a reliable upgrade that’s worth the small investment—easy to install, sturdy, and effective in protecting my equipment.
What is a Vacuum Valve and Why is it Important?
A vacuum valve is a device used to control the flow of gases in a vacuum system by either allowing or preventing the passage of gas. It plays a critical role in maintaining the integrity of vacuum conditions by managing pressure differences within the system. Vacuum valves can be found in various applications, including industrial processes, scientific research, and manufacturing, where maintaining a specific atmospheric condition is essential.
According to the American Vacuum Society, vacuum valves are fundamental components in systems that require precise control over gas flow and pressure (American Vacuum Society). They are essential in preventing contamination, managing pressure levels, and ensuring that vacuum systems operate efficiently and effectively.
Key aspects of vacuum valves include their types—such as gate, ball, butterfly, and check valves—each designed for specific applications and pressure ranges. The materials used in manufacturing vacuum valves are also crucial; they must withstand the corrosive effects of various gases and maintain sealing integrity at low pressures. Additionally, the design and mechanism of the valve can significantly influence its performance, including factors like opening time, wear resistance, and flow capacity.
The importance of vacuum valves extends beyond mere gas flow control; they also significantly impact the efficiency and reliability of vacuum systems. For instance, in semiconductor manufacturing, the presence of contaminants can lead to defective products, making the use of high-quality vacuum valves paramount. Furthermore, in scientific research, vacuum systems are often used in experiments that require an ultra-clean environment, where even minute quantities of gas can alter results.
Statistics indicate that industries utilizing vacuum systems contribute significantly to the global economy, with the semiconductor industry alone expected to reach a market value of over $500 billion by 2027 (Research and Markets). As demand for precision and efficiency continues to rise, the importance of high-performance vacuum valves becomes even more critical in maintaining competitive advantages.
The benefits of using the best vacuum valves include improved system reliability, enhanced process consistency, and extended equipment life. To ensure optimal performance, it is essential to select the right type of valve for specific applications, regularly maintain and calibrate valves, and monitor the vacuum system for leaks or failures. Best practices include using high-quality materials, employing appropriate sealing technologies, and implementing robust maintenance schedules to prolong the life of both the valves and the vacuum systems they serve.
How Does a Vacuum Valve Work in a System?
A vacuum valve is a vital component in vacuum systems that controls the flow of gases and maintains the desired vacuum level.
- Types of Vacuum Valves: Different types of vacuum valves include gate valves, ball valves, and butterfly valves, each designed for specific applications and pressure ranges.
- Function: The primary function of a vacuum valve is to regulate the passage of gas, either allowing or restricting flow to maintain the vacuum conditions.
- Actuation Mechanisms: Vacuum valves can be actuated manually, electrically, or pneumatically, which determines how they open and close in response to system demands.
- Material Selection: The materials used in vacuum valves must withstand corrosive environments and extreme pressure differentials, commonly utilizing metals like stainless steel or specialized plastics.
- Sealing Mechanisms: Effective sealing is crucial in vacuum valves, and various sealing methods, such as elastomeric seals or metal-to-metal seals, are employed to prevent leaks.
- Applications: Vacuum valves are used in a wide range of applications, including semiconductor manufacturing, research laboratories, and industrial processes requiring precise vacuum control.
Types of Vacuum Valves: Different types of vacuum valves include gate valves, ball valves, and butterfly valves, each designed for specific applications and pressure ranges. Gate valves are often used in high vacuum systems, while ball valves offer quick shut-off capabilities, and butterfly valves are suitable for large volume applications where space is a constraint.
Function: The primary function of a vacuum valve is to regulate the passage of gas, either allowing or restricting flow to maintain the vacuum conditions. By opening or closing, the valve can either introduce new gases into the system or maintain the existing vacuum, ensuring optimal performance of the vacuum system.
Actuation Mechanisms: Vacuum valves can be actuated manually, electrically, or pneumatically, which determines how they open and close in response to system demands. Electric actuators provide precise control, while pneumatic actuators can offer faster response times, making the choice of actuation critical based on the application.
Material Selection: The materials used in vacuum valves must withstand corrosive environments and extreme pressure differentials, commonly utilizing metals like stainless steel or specialized plastics. The choice of material also affects the valve’s performance at different temperatures and its longevity under varying operational conditions.
Sealing Mechanisms: Effective sealing is crucial in vacuum valves, and various sealing methods, such as elastomeric seals or metal-to-metal seals, are employed to prevent leaks. The effectiveness of the seal directly impacts the efficiency of the vacuum system, as any leaks can result in loss of vacuum and reduced performance.
Applications: Vacuum valves are used in a wide range of applications, including semiconductor manufacturing, research laboratories, and industrial processes requiring precise vacuum control. Their ability to maintain stable vacuum conditions is essential for the integrity of processes such as thin-film deposition and material characterization.
What Are the Different Types of Vacuum Valves Available?
The different types of vacuum valves available include:
- Gate Valves: Gate valves are designed to provide a straight-through flow path with minimal resistance, making them ideal for applications that require a high flow rate.
- Butterfly Valves: Butterfly valves utilize a rotating disc to control the flow, offering a compact design that is suitable for systems with limited space and is efficient for quick shut-off.
- Ball Valves: Ball valves feature a spherical disc that rotates to open or close the flow, providing a reliable sealing mechanism and are favored for their durability and ease of operation.
- Diaphragm Valves: Diaphragm valves use a flexible diaphragm to regulate flow, which allows for excellent sealing and isolation, making them suitable for applications involving corrosive materials.
- Check Valves: Check valves allow flow in one direction only, preventing backflow and ensuring that the vacuum system maintains its integrity during operation.
- Pneumatic Actuated Valves: These valves are operated by pneumatic pressure, allowing for remote control and automation, which is beneficial in complex vacuum systems for precise flow management.
- Solenoid Valves: Solenoid valves use an electromagnetic coil to open or close the valve, providing rapid actuation and enabling automated control in various vacuum applications.
Gate valves are particularly effective in applications requiring minimal pressure loss, as they allow for a clear passage when fully open. They are often used in larger pipelines and systems where flow efficiency is essential.
Butterfly valves are advantageous for their lightweight construction and quick operation, often used in HVAC and industrial processes. Their design minimizes the pressure drop across the valve, making them efficient in controlling flow rates.
Ball valves are known for their versatility and reliability, providing a tight seal that prevents leaks, making them suitable for high-pressure applications. They are commonly used in water, oil, and gas systems due to their robustness.
Diaphragm valves are particularly useful in applications where contamination must be avoided, as the diaphragm isolates the flow from the actuator. This feature makes them ideal for pharmaceutical and food processing industries.
Check valves are crucial in maintaining system integrity by preventing backflow, which can cause contamination or damage. They are widely used in pumps and vacuum systems to ensure proper operation.
Pneumatic actuated valves are integral in automated systems where quick and precise control is necessary. They are often used in industrial processes to enhance efficiency and reduce manual intervention.
Solenoid valves are ideal for applications requiring fast and frequent switching, as they can be controlled electronically. Their reliability and speed make them popular in automated vacuum systems and robotics.
What Are the Benefits of Using a Diaphragm Vacuum Valve?
The benefits of using a diaphragm vacuum valve include enhanced control, durability, and reduced contamination.
- Precise Control: Diaphragm vacuum valves offer excellent flow control, allowing for fine adjustments in vacuum levels and pressures. This precision is crucial in applications requiring a stable vacuum environment, such as in chemical processing and semiconductor manufacturing.
- Durability: These valves are designed with robust materials that withstand harsh operating conditions. Their construction minimizes wear and tear over time, leading to longer service life compared to other valve types, which is particularly beneficial in high-frequency cycling applications.
- Reduced Contamination: The design of diaphragm valves helps prevent contamination of the working environment. The diaphragm acts as a barrier, isolating the valve mechanism from the process fluid, which is essential in industries where purity is paramount, such as pharmaceuticals and food processing.
- Low Maintenance: Diaphragm vacuum valves typically require less maintenance than other types of valves. Their simple design and fewer moving parts lead to reduced likelihood of failure and lower operational costs over time.
- Versatility: These valves are versatile and can be used in a wide range of applications, from laboratory settings to large-scale industrial processes. Their adaptability makes them suitable for various gases and vapors, enhancing their usability across different sectors.
What Makes Gate Vacuum Valves Unique?
Gate vacuum valves are known for their unique design and functionality in vacuum systems.
- Sealing Mechanism: Gate vacuum valves utilize a flat gate that moves to seal the flow path, which provides a tight seal when closed and reduces leakage significantly.
- Low Conductance: These valves typically have low conductance when closed, which minimizes the impact on the vacuum system’s performance by preventing gas flow.
- Minimal Particle Generation: The design of gate valves reduces the potential for particle generation during operation, making them suitable for sensitive applications such as semiconductor manufacturing.
- Robust Construction: Gate vacuum valves are often constructed from durable materials, allowing them to withstand high vacuum environments and extreme conditions without degradation.
- Manual and Automated Operation: They can be operated manually or automatically, providing flexibility in various system designs and allowing for integration with automated processes.
The sealing mechanism of gate vacuum valves is particularly effective because the flat gate compresses against a seat, creating a barrier that prevents gas from passing through when closed. This characteristic is essential for maintaining the integrity of the vacuum environment.
Low conductance is another hallmark of gate valves; when they are in the closed position, they restrict gas flow significantly, which helps maintain the desired vacuum levels in the system without introducing unnecessary gas load.
A key advantage of gate vacuum valves is their minimal particle generation, which is crucial in high-purity applications. This is due to their simple design that avoids complex moving parts that can shed particles during operation.
The robust construction of these valves means they are made from high-quality materials such as stainless steel, which can endure the harsh conditions of high vacuum environments, ensuring longevity and reliability in operation.
Finally, gate vacuum valves offer the versatility of manual and automated operation. This allows them to be easily integrated into various vacuum systems, accommodating both user-controlled and automated processes for enhanced efficiency.
When Should You Use a Knife Vacuum Valve?
A knife vacuum valve is typically used in scenarios involving vacuum systems where precise control of vacuum pressure is required, particularly in industrial and laboratory settings.
- Vacuum Sealing: Knife vacuum valves are ideal for vacuum sealing applications where maintaining a consistent vacuum level is essential to preserve the integrity of the contents. These valves allow for quick opening and closing, enabling efficient sealing processes.
- Material Transfer: In processes that involve transferring materials under vacuum conditions, knife vacuum valves help to minimize contamination and maintain the purity of the materials being handled. Their design allows for safe and effective isolation of different stages of the transfer process.
- Process Control: These valves are beneficial in systems requiring precise control over pressure and vacuum levels. By using a knife vacuum valve, operators can easily adjust the vacuum level, which is critical in processes like distillation or chemical reactions where pressure variations can affect outcomes.
- Maintenance and Cleanup: Knife vacuum valves facilitate easier maintenance and cleaning of vacuum systems. Their design allows for simple disassembly, which is crucial for preventing cross-contamination and ensuring that the system operates efficiently.
- High-Temperature and Corrosive Applications: In environments where high temperatures or corrosive substances are present, knife vacuum valves made from durable materials can withstand harsh conditions. This resilience ensures longevity and reliability in demanding applications.
What Factors Should You Consider When Choosing the Best Vacuum Valve?
When choosing the best vacuum valve, several critical factors should be considered to ensure optimal performance and suitability for your specific application.
- Material Compatibility: The vacuum valve must be made from materials that are compatible with the substances it will come into contact with. Considerations such as chemical resistance, temperature stability, and potential for corrosion are vital to avoid premature failure or contamination.
- Pressure Rating: The valve should have a pressure rating that meets or exceeds the operating conditions of your system. This ensures that the valve can withstand the vacuum levels required without risking failure or leakage, which could compromise the system’s performance.
- Actuation Type: Vacuum valves can be actuated manually, electrically, or pneumatically. The choice of actuation type affects the ease of use, response time, and integration with automation systems, so it’s essential to select one that aligns with your operational needs.
- Flow Characteristics: Different valves have varying flow characteristics, which can impact the efficiency of your vacuum system. It’s important to choose a valve that provides optimal flow for your application, minimizing restrictions that could affect overall performance.
- Size and Port Configuration: The size of the vacuum valve and its port configuration must be compatible with the existing piping or equipment. Ensuring proper sizing helps maintain system integrity and prevents bottlenecks in the vacuum flow.
- Maintenance Requirements: Consider the maintenance needs of the valve, including how easy it is to clean or replace components. A valve that requires less frequent maintenance can lead to lower operational costs and less downtime.
- Cost and Value: While it may be tempting to choose the least expensive option, it’s important to evaluate the overall value of the vacuum valve. Factors such as durability, warranty, and manufacturer reputation can affect long-term costs and reliability.
How Do Material and Build Quality Affect Vacuum Valve Performance?
The performance of vacuum valves is significantly influenced by the material and build quality. High-quality materials can enhance durability, resistance to wear, and overall efficiency. Here’s how they play a crucial role:
-
Material Composition: Common materials include stainless steel, brass, and specialized polymers. Stainless steel valves, for instance, offer excellent corrosion resistance and longevity, making them ideal for demanding environments. In contrast, Teflon-coated valves can provide superior chemical resistance, which is critical in applications involving aggressive substances.
-
Build Quality: The precision of manufacturing affects the valve’s leak tightness and flow characteristics. Well-engineered valves minimize gaps that could lead to inefficiencies. For instance, precision-machined components ensure smooth operation and enhance vacuum integrity, while inferior construction might result in increased maintenance costs over time.
-
Temperature and Pressure Ratings: Materials with higher thermal stability can handle extreme conditions without degrading. For example, aluminum valves are lightweight but may not withstand high temperatures as effectively as other materials.
By selecting vacuum valves that excel in both material and build quality, users can ensure reliable operation and optimal system performance in various applications.
Why is Valve Size Critical for Optimal Functionality?
Furthermore, the interaction between valve size and system design is also significant. For instance, a well-sized valve allows for proper modulation of gas flow, which is essential for processes requiring precise vacuum levels. Studies have shown that improperly sized valves can lead to cavitation and wear, ultimately affecting the durability and reliability of the system (Journal of Vacuum Science & Technology, 2023). Understanding these causal relationships helps in selecting the best vacuum valve for specific applications, ensuring optimal performance and efficiency.
Which Brands are Recognized as Leaders in Vacuum Valves?
When it comes to vacuum valves, several brands are recognized for their quality, innovation, and reliability. These leaders have established themselves in various industries, providing high-performance solutions for both commercial and industrial applications.
-
Parker Hannifin: Known for its extensive range of vacuum valves, Parker offers durable and versatile products suitable for semiconductor manufacturing, packaging, and other high-tech environments.
-
Swagelok: This brand specializes in fluid system components, including vacuum valves that are designed for precision and safety in rigorous processes, ensuring leakage-free performance.
-
Valex: Valex focuses on the semiconductor market, providing high-purity vacuum valves that meet stringent cleanliness requirements, ensuring minimal contamination in critical processes.
-
Lesker Company: Recognized for their advanced vacuum technology, Lesker manufactures a diverse array of valves suitable for research and development, as well as production in vacuum systems.
-
Kurt J. Lesker Company: Their range includes automated and manual vacuum valves, catering to a variety of industries including pharmaceuticals and aerospace.
These brands are noted for their commitment to quality and customer satisfaction, making them go-to options when selecting vacuum valves for various applications.
What Are the Common Applications of Vacuum Valves Across Industries?
Vacuum valves have a wide range of applications across various industries due to their ability to control gas flow in vacuum systems.
- Semiconductor Manufacturing: Vacuum valves are essential in the fabrication of semiconductor devices, where maintaining a controlled environment is crucial. They help in the deposition and etching processes by enabling the precise control of gases and maintaining the required vacuum levels.
- Pharmaceuticals: In the pharmaceutical industry, vacuum valves are used in processes such as drying, sterilization, and packaging. They ensure that products are processed in a contaminant-free environment, which is vital for maintaining the integrity and efficacy of medications.
- Food Packaging: Vacuum valves play a key role in food preservation by enabling vacuum sealing processes. This helps in extending the shelf life of food products by removing air, which can lead to oxidation and spoilage.
- Aerospace: In aerospace applications, vacuum valves are utilized in testing and manufacturing components, particularly for systems that require vacuum conditions to simulate space environments. They are critical for ensuring the reliability and performance of aerospace technologies.
- Research and Development: Many laboratories utilize vacuum valves in experimental setups, particularly in physics and chemistry research. They allow researchers to create controlled environments for experiments, such as studying materials under vacuum conditions or conducting vacuum distillation.
- HVAC Systems: In heating, ventilation, and air conditioning (HVAC) systems, vacuum valves are employed to manage the flow of refrigerants and gases. They help in optimizing system performance and energy efficiency by maintaining the necessary vacuum levels.
What Insights Do Customer Reviews Provide About Popular Vacuum Valves?
Customer reviews provide valuable insights into the performance, reliability, and user experience of popular vacuum valves.
- Performance: Customers often share their experiences regarding how well a vacuum valve performs under different conditions. This includes feedback on how effectively the valve maintains vacuum pressure and whether it operates smoothly without leaks.
- Durability: Reviews frequently highlight the longevity of vacuum valves, noting any issues with wear and tear over time. Users may discuss materials used in the construction of the valve and whether they hold up against regular use and environmental factors.
- Installation Ease: Many reviews detail the installation process of vacuum valves, indicating whether they are user-friendly or require specialized tools and skills. Feedback on installation can influence potential buyers’ decision-making, especially for those looking for DIY solutions.
- Customer Support: Insights regarding the manufacturer’s customer service can be crucial, as users often report their experiences with warranty claims or technical assistance. Positive experiences with customer support can enhance a product’s reputation, while negative experiences may deter potential buyers.
- Value for Money: Reviews typically include discussions about the cost of vacuum valves relative to their performance and features. Customers often weigh the benefits they received against the price paid, helping others assess whether a particular valve is worth the investment.
- Noise Levels: Some customers comment on the noise produced by vacuum valves during operation. This aspect can be particularly important for users in noise-sensitive environments, and reviews may help identify quieter models that still perform effectively.
What Common Mistakes Should You Avoid When Buying a Vacuum Valve?
When purchasing a vacuum valve, avoiding common mistakes can ensure you select the best option for your needs.
- Not Considering the Application: It is crucial to understand the specific application for which the vacuum valve will be used. Different applications require different types of valves, such as gate valves for isolation or check valves for preventing backflow, and failing to match the valve type to your application can lead to inefficiency or failure.
- Ignoring Material Compatibility: The materials used in the construction of the vacuum valve should be compatible with the substances they will encounter. For example, corrosive chemicals require valves made from resistant materials like stainless steel or specific plastics, and using the wrong material can result in damage and leaks.
- Overlooking Size and Specifications: Selecting a vacuum valve that does not fit the system’s size and pressure specifications can cause operational issues. It is important to measure the pipe diameter and ensure the valve can handle the required pressure and vacuum levels to function correctly.
- Failing to Check for Certification Standards: Vacuum valves should meet industry standards and certifications for safety and performance. Skipping this step can lead to non-compliance with regulations, which can be costly and dangerous in industrial settings.
- Neglecting Maintenance Requirements: Some vacuum valves require regular maintenance to ensure optimal performance. Not considering the maintenance needs can lead to unexpected downtime and repair costs, so understanding the valve’s maintenance requirements is essential for long-term reliability.
- Choosing Based on Price Alone: While budget is a factor, choosing a vacuum valve solely based on price can lead to subpar performance or premature failure. It is important to evaluate the overall value, including quality, reliability, and warranty, rather than just the initial cost.